 This article explores how acid fume scrubbers contribute to safer, more compliant industrial environments by neutralizing hazardous chemical vapors in chemical, pharmaceutical, fertilizer, and semiconductor production facilities.
Table of Contents
- Introduction
- Managing Acid Fumes: The Industrial Challenge
- How Acid Fume Scrubbers Work
- Industry-Specific Applications
- Addressing Operational Requirements
- Choosing the Right Solution Provider
- Conclusion & Next Steps
- FAQs
1. Introduction
Facility managers face a hidden yet costly hazard every day. Airborne acid fumes in chemical manufacturing, pharmaceutical production, and fertilizer industries quietly harm workers, corrode valuable equipment, and trigger costly regulatory violations. Left uncontrolled, these corrosive vapors threaten operational efficiency, equipment integrity, and the financial bottom line. Acid fume scrubbers protect your facility by capturing, neutralizing, and safely disposing of harmful vapors before they spread. The measurable benefits include:- Lower risk of worker injury and improved health outcomes
- Extended the lifespan of critical equipment by reducing corrosion
- Reduced maintenance costs and downtime related to vapor damage
- Simplified compliance with OSHA and EPA regulations, preventing costly penalties
2. Managing Acid Fumes: The Industrial Challenge
Manufacturing facilities within the chemical, pharmaceutical, and fertilizer industries routinely handle highly corrosive chemicals that generate hazardous vapors, including sulfuric, hydrochloric, nitric, and hydrofluoric acids. Common sources of acid fumes include:- Chemical etching and processing areas
- Mixing and reaction vessels
- Storage tank venting units
- Material transfer operations
- Quality control labs
- Waste treatment systems
- Worker Health Risks: Airborne acid vapors cause immediate respiratory irritation and, over time, can lead to severe conditions such as chemical burns, chronic respiratory disease, and occupational asthma.
- Equipment Corrosion: Acid fumes aggressively attack metal surfaces, electrical components, and structural parts, leading to faster equipment degradation, higher maintenance costs, and unplanned downtime.
- Increasing Regulatory Pressure: Facilities without proper vapor control risk hefty OSHA and EPA fines, production shutdowns, and costly litigation.
3. How Acid Fume Scrubbers Work
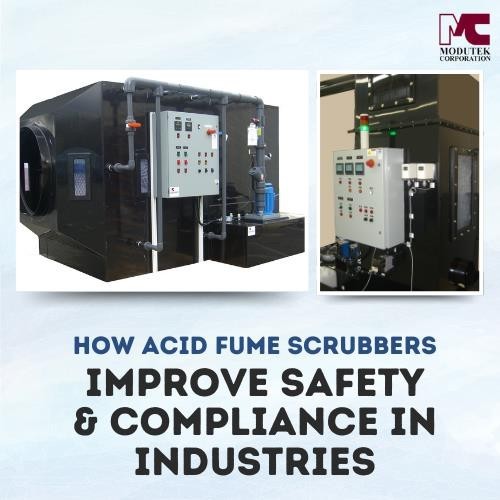
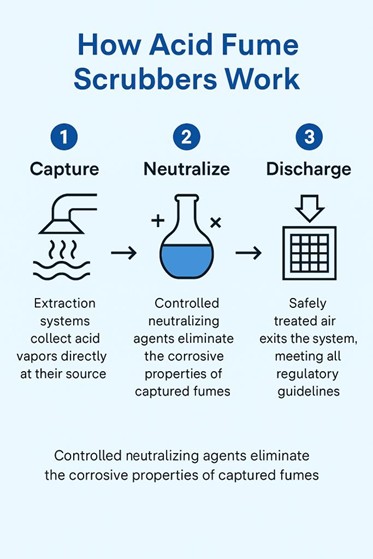
Acid fume scrubbers are specially engineered systems that effectively capture and neutralize harmful vapors. In simple terms, they convert dangerous airborne acids into clean, compliant exhaust through a clear three-step process:- Capture:Extraction systems collect acid vapors directly at their source.
- Neutralize:Controlled neutralizing agents eliminate the corrosive properties of captured fumes.
- Discharge:Safely treated air exits the system, meeting all regulatory guidelines.
 Two primary types of scrubber systems are commonly used based on facility needs:
- Two-Stage Systems: Ideal for moderate concentrations, these systems capture particulates and perform initial vapor neutralization before fully neutralizing and discharging cleaned air.
- Three-Stage Systems: Designed for high concentrations or hazardous acids, adding an extra stage provides enhanced neutralization capacity and greater compliance assurance.
- Digital pH Monitoring: Real-time tracking ensures optimal neutralization efficiency, minimizing manual oversight and guesswork.
- Automatic Adjustment: Reagent flow rates dynamically adjust to maintain proper chemical balance despite changing conditions.
- Programmable Logic Controllers (PLCs): Provide continuous monitoring, enabling facility managers to identify and resolve anomalies promptly.
4. Industry-Specific Applications
4.1 Chemical Manufacturing
Industry Challenges: Chemical manufacturers face particularly demanding acid fume management requirements. Frequent use of corrosive substances like sulfuric and hydrochloric acid throughout production processes creates persistent vapor hazards. These aggressive chemicals accelerate equipment degradation, increase worker exposure risks, and can trigger serious environmental violations if not adequately controlled. Benefits of Acid Fume Scrubbers: Properly designed scrubber systems capture and neutralize corrosive vapors at their source, creating multiple operational advantages. By preventing fumes from spreading throughout the facility, these systems significantly reduce corrosion-related maintenance expenses while extending equipment lifespan. Worker safety improves dramatically as respiratory hazards diminish. Reliable fume control also helps ensure continuous compliance with increasingly strict OSHA and EPA requirements. Key Features in Modutek’s Fume Scrubbers:- Fully Automatic Operation: Ensures consistent treatment of acidic waste streams without requiring constant human oversight—vital in high-risk environments where even minor exposure can cause serious harm.
- Microprocessor-Based pH Control: offers precision critical for neutralizing powerful chemical vapors, reducing the risk of under- or over-treatment, which can lead to compliance issues or equipment wear.
- Touchscreen PLCs with Alarm Systems: provide real-time pH data and immediate alerts for anomalies, enabling quick intervention and minimizing personnel exposure risks.
4.2 Pharmaceutical Production
Industry Challenges: Pharmaceutical facilities operate under stringent quality standards. Cleanrooms and R&D environments demand ultra-high air quality, where even trace acid vapors can compromise product purity, invalidate research outcomes, or trigger non-compliance with FDA standards. The stakes are particularly high given the value of pharmaceutical products and research investments. Benefits of Acid Fume Scrubbers: Specialized scrubber systems prevent contamination by effectively removing vaporized acids in compound synthesis or lab-scale manufacturing processes. This protection maintains the integrity of controlled environments, ensures consistent product quality, and supports regulatory compliance requirements. Key Features in Modutek’s Fume Scrubbers:- Compact Design with Double Containment: Ideal for space-constrained environments where cleanliness and leak prevention are paramount. Double containment adds a layer of safety that meets pharmaceutical facility design standards.
- High-Accuracy pH Sensors: Ensure neutralization processes meet exacting standards, which is essential in validated environments where even minor chemical residue can trigger audits or shutdowns.
- Digital Chart Recorder: Provides continuous documentation for regulatory audits and internal quality assurance—a critical asset in pharmaceutical manufacturing and R&D compliance frameworks.
4.3 Fertilizer Industry
Industry Challenges: Fertilizer production typically involves handling large volumes of ammonia and acidic byproducts. These processes generate significant vapor concentrations that pose serious worker safety risks and create potential regulatory issues related to air quality and emissions. Production scale often magnifies these challenges. Benefits of Acid Fume Scrubbers: Industrial-grade acid fume scrubbers efficiently remove hazardous fumes from production areas, protecting workers while helping companies maintain environmental compliance. By controlling emissions at the source, these systems prevent both acute exposure incidents and long-term environmental impact. Key Features in Modutek’s Fume Scrubbers:- UV-Rated Outdoor-Ready Systems: Designed to withstand harsh outdoor conditions typical of fertilizer production sites. This ensures reliable operation without degradation due to UV or weather exposure.
- Three-Stage Systems: Tailored for heavy-duty applications involving high concentrations of acidic gases. Multiple stages ensure complete neutralization, supporting worker safety and emission control.
- Dual Metering Pumps per Stage: Deliver precise chemical dosing across high flow rates—critical for large-scale production environments where dosing errors can compromise the entire neutralization process.
4.4 Semiconductor Wafer Processing
Industry Challenges: semiconductor wet bench processes that etch, strip, or clean silicon wafers with acids generate acid mist in the process station exhaust. That exhaust can’t be released into the workspace because acid droplets create health risks for workers and corrode sensitive equipment, and worker safety standards and environmental regulations limit permissible acid droplet concentration. Semiconductor manufacturing depends on a clean, particle-free process space, so any acid exhaust event that puts that at risk carries real yield and safety consequences on top of standard OSHA and EPA exposure limits. Benefits of Acid Fume Scrubbers: Acid fume scrubbers remove acid droplets from the process discharge air so it’s clean enough to release into the workspace or outside, keeping the workspace safe for employees and the surrounding environment free of acid contamination. Because almost all acid is removed once the scrubber’s flow capacity matches the wet process station’s exhaust, scrubbers can be sized precisely to a fab’s actual throughput rather than over- or under-specified. Key Features in Modutek’s Fume Scrubbers:- Stand-Alone or Integrated Configurations: available as a stand-alone acid fume scrubber, built directly into an existing wet bench station, or specified as part of a complete production line.
- High-Surface Lantec Packing Materia: maximizes acid mist absorption as it passes over the packed scrubber bed, removing up to 99 percent of acid mist.
- Flow Capacities from 500 to 25,000 CFM: covers everything from a small research lab facility to large-volume manufacturing lines.
5. Addressing Operational Requirements
Effective acid fume control means choosing scrubber systems tailored precisely to your facility’s unique operational needs. Different production volumes, acid concentrations, and facility layouts require specific capabilities. Modutek designs systems with flexible sizing, safety-focused engineering, and automation features specifically targeted to these critical factors. Flexible System Sizing Your production size determines the required scrubber capacity. Modutek offers modular system designs ranging from 5 GPM (ideal for labs and smaller applications) up to 500 GPM for large-scale industrial needs. This adaptability ensures:- Systems precisely match existing production needs.
- Expansion capability as operations grow.
- Reliable performance during peak productivity times.
- Smooth operation during maintenance or equipment transitions.
- UV-Resistant Materials: Prevent damage from continued sun exposure.
- Weatherproof Control Enclosures: Extend the lifespan and reliability of critical electronics.
- Temperature-Compensated Components: Sustain high-performance operation in harsh climates.
- Robust Construction: withstand environmental stress without losing efficiency.
- PLC Controls: Maintain precise scrubber function without hands-on intervention.
- Ethernet Connectivity: Allows remote performance monitoring, reducing onsite workload.
- Automated Alarms: Provide immediate notification of any anomalies or performance deviations.
- Remote Monitoring Capabilities: Enable oversight from anywhere within or outside your facility.
- Operator Interface Instrumentation: pressure gauges, flow meters, and water level indicators with discharge metering give operators a full real-time picture of scrubber status alongside the PLC automation above.
- Optimized chemical dosing for accurate neutralization control.
- Redundant key components to prevent downtime due to a single-point failure.
- Accurate real-time monitoring ensuring regulatory compliance.
- Simplified maintenance procedures designed to minimize downtime.
6. Choosing the Right Solution Provider
Selecting an acid fume scrubber system involves more than evaluating equipment specs alone. The provider’s industry expertise, customization capability, and long-term support are equally crucial, as improper vapor control can lead to costly downtime, regulatory fines, or safety incidents. Facility managers must carefully consider these key factors: Industry Experience and Expertise Providers with deep industry-specific knowledge offer important advantages, ensuring:- Compliance with OSHA, EPA, and FDA industry standards
- Effective handling of your common chemical types and concentrations
- Solutions built to handle your facility’s unique operational processes
- Facility layout and available space
- Production volume and peak capacity needs
- Required integration with existing equipment and infrastructure
- Automation and real-time monitoring preferences
- Timely installation and system commissioning
- Availability of responsive maintenance programs
- Reliable spare parts delivery
- Easy access to expert technical support when needed
- Flexible upgrade options aligned with facility growth and regulatory changes
7. Conclusion & Next Steps
Proper acid fume management offers significant operational advantages for facility managers across chemical manufacturing, pharmaceutical production, and fertilizer industries. Acid fume scrubbers directly contribute to stronger performance and reduced expenses by delivering clear benefits, including:- Improved Worker Safety by eliminating respiratory hazards and protecting against long-term health impacts.
- Extended Equipment Lifespan by effectively preventing corrosive damage.
- Significantly Reduced Maintenance Costs and minimized unexpected downtime.
- Reliable regulatory compliance, keeping facilities aligned with OSHA and EPA, and strict industry guidelines.
- Greater operational efficiency is achieved through intelligent automation and precise monitoring.
- Detailed needs assessment and system specification
- Custom design engineering to match your exact requirements
- Professional installation and commissioning
- Operator training and documentation
- Ongoing technical support and service
8. FAQs
How Acid Fume Scrubbers Improve Safety & Compliance in Industries
What airflow capacity range do Modutek’s acid fume scrubbers support?
Modutek acid fume scrubbers handle 500 to 25,000 CFM, from small research labs to high-volume manufacturing lines. When the scrubber’s flow capacity matches the wet process station’s exhaust, almost all of the acid is removed.
How effective are the scrubbers at removing acid mist?
They use a wet-packed bed of high-surface-area Lantec packing material with a recirculating neutralizing solution. This design removes up to 99 percent of acid fume chemicals from the exhaust stream.
Can a scrubber be integrated into an existing wet bench?
Yes. A scrubber can be supplied as a stand-alone unit, built directly into a wet bench station, or specified as part of a complete production line.
What controls help operators check performance and document compliance?
Standard features include:
- pH control of the recirculating water
- flow and pressure gauges
- water level control
- metered water discharge
Automation options include PLC controls with alarms, Ethernet connectivity for remote monitoring, and a digital chart recorder for continuous records. The controls sit in a NEMA 4 cabinet.
Are the scrubbers suitable for outdoor installation, and what certifications are available?
The scrubbers are built from black polypropylene with UV protection and have a double-containment design. Structural and seismic certification is available when specified. Modutek designs equipment to recognized compliance standards, including UL/ETL for industrial control panels and NFPA 79. Third-party evaluations, such as Structural PE and Seismic PE, are quoted as options.
How much water does a scrubber consume?
Very little. The neutralizing solution is recirculated instead of continuously drained, and a bottom drain makes routine maintenance easier.
Where are the scrubbers built, and what support is available after installation?